An Ultra high purity chemical delivery system is a specialized infrastructure developed to store, transportation, control, and supply extremely cleansed chemicals to producing procedures. These systems are engineered to safeguard chemical top quality throughout the entire shipment course. In markets such as semiconductor production, pharmaceuticals, biotechnology, and progressed materials, even very small amounts of contamination can affect production results. For this reason, system style focuses on tidiness, material compatibility, managed flow, and trustworthy procedure.
Relevance of Maintaining Chemical Pureness
Chemical purity plays a vital role in modern-day industrial production. Production processes typically depend upon carefully regulated chemical structures, concentrations, and circulation rates. Unwanted fragments, dampness, steels, or other contaminants can hinder delicate processes and possibly decrease product consistency. An Ultra high purity chemical delivery system helps reduce these risks by using thoroughly selected components and controlled handling procedures. Keeping purity from storage with point-of-use distribution supports secure production and assists suppliers meet requiring process specs.
Essential System Elements
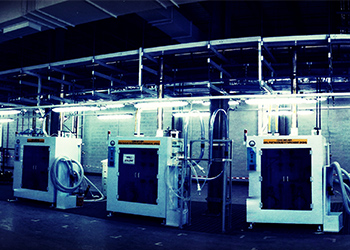
A full chemical distribution remedy may consist of storage space containers, piping, valves, filters, pumps, regulators, sensors, and specialized installations. Each part needs to work with the chemicals included and appropriate for the called for pureness level. Interior surfaces are commonly made to decrease fragment generation and chemical interaction. High-grade connections and seals can likewise help reduce leakage and contamination. Relying on the application, systems may be set up for central distribution or straight point-of-use distribution, offering flexibility for various center layouts and manufacturing demands.
Precision Flow and Refine Control
Accurate chemical shipment calls for mindful monitoring of pressure, circulation, temperature level, and various other operating problems. Modern systems can integrate automatic valves, electronic sensors, circulation controllers, and monitoring systems to maintain consistent distribution. Automation lowers the requirement for unneeded hands-on intervention and allows operators to observe vital system criteria in actual time. A properly developed Ultra high purity chemical delivery system can for that reason add to repeatable processing and improved operational control, particularly where manufacturing tolerances are exceptionally demanding. Go to this web site https://www.chengweisemi.com/application/ about to know a lot more.
Safety And Security and Preventive Upkeep
Handling high-purity chemicals needs interest to both item honesty and office safety and security. Ideal control, ventilation, leakage discovery, pressure controls, and emergency situation closure devices can help reduce operational threats. Precautionary upkeep is another important factor to consider. Routine assessments can identify worn seals, damaged tubes, stopped up filters, or malfunctioning valves prior to they impact production. Cleansing and substitute procedures must be carried out according to established specifications. In-depth upkeep documents can likewise support top quality management, traceability, and lasting system reliability.

Future Trends in Chemical Distribution Modern Technology
The advancement of innovative production is creating brand-new demands for chemical delivery framework. Future systems are anticipated to increasingly integrate electronic monitoring, automation, anticipating maintenance, and enhanced materials. Linked sensing units can offer details about circulation, stress, temperature, and system performance, enabling drivers to recognize uncommon problems faster. As manufacturing procedures come to be much more specific, the Ultra high purity chemical delivery system will remain to provide a vital structure for regulated chemical circulation. Combining premium products, accurate procedure control, automation, and consistent maintenance can aid markets accomplish trusted efficiency while protecting chemical pureness throughout manufacturing.